24/7 Phone Services
-
-
Visit Our Place
S. G. Highway, Ahmedabad - 380051
Pressure Swing Adsorption Plant: 7 Powerful Benefits for Efficient Gas Separation
Pressure Swing Adsorption Plant (PSA) is an efficient gas separation technology used for oxygen generation, nitrogen production, hydrogen purification and industrial gas applications.
Table of Contents
- Introduction to PSA Technology
- What Is a PSA Plant?
- Main Components of a PSA Plant
- How Does a PSA Plant Work?
- PSA Plant Process Flow
- Types of PSA Plants
- Key Advantages of PSA Technology
- Factors Affecting PSA Plant Performance
- PSA Plant Maintenance
- PSA Plant Safety Considerations
- Industrial Applications of PSA Technology
- How to Select the Right PSA Plant
- Importance of Automation in PSA Plants
- Frequently Asked Questions About PSA Plants
- Conclusion
Introduction to PSA Technology
A PSA Plant (Pressure Swing Adsorption Plant) is an advanced gas separation and purification system used in various industrial applications for producing or purifying gases such as oxygen, nitrogen, hydrogen and methane-rich gas. PSA technology works on the principle of selective adsorption, where a specially selected adsorbent material captures particular components of a gas mixture under pressure while allowing the required gas to pass through.
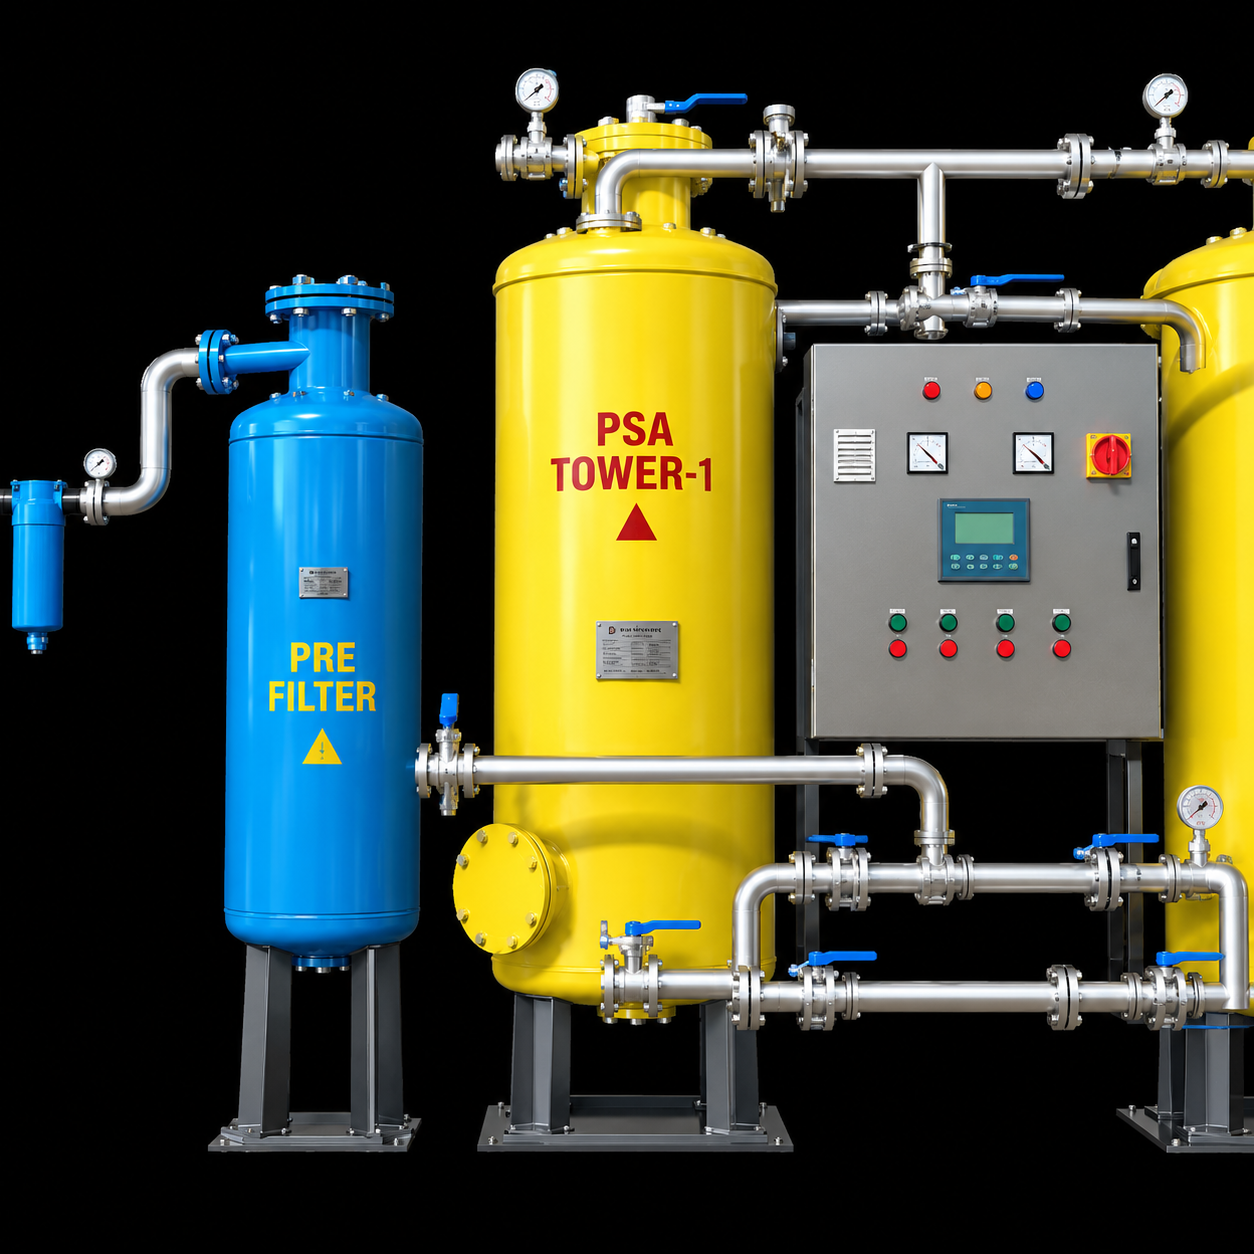
The industrial PSA system shown in the image consists of important components such as a pre-filter, adsorption vessel, process piping, automatic valves, pressure gauges, control panel and supporting equipment. All these components work together to provide controlled and efficient gas separation. The exact arrangement of a PSA system can vary depending on the type of gas being produced, required purity, flow capacity, feed-gas composition and operating pressure.
PSA technology has become an important solution for industries that require an on-site and reliable supply of industrial gases. Instead of depending completely on externally supplied gas cylinders or other traditional supply methods, a properly designed PSA system can generate the required gas at the location where it is needed.
The technology is based on a cyclic process. During one part of the cycle, the adsorption material operates under increased pressure and selectively adsorbs unwanted gas components. During another part of the cycle, pressure is reduced and the adsorbent is regenerated. Multiple adsorption vessels can be operated in sequence so that the overall plant can provide a continuous product-gas supply.
Introduction to Pressure Swing Adsorption
Pressure Swing Adsorption, commonly abbreviated as PSA, is a gas separation technology that uses differences in the adsorption characteristics of gases. When a gas mixture comes into contact with a suitable adsorbent at a particular pressure, some components are retained more strongly than others. By controlling the pressure, the adsorbed components can later be released and the adsorbent can be regenerated.
The basic concept is relatively simple, but the design of an industrial PSA plant requires careful engineering. The adsorption material, vessel dimensions, operating pressure, valve arrangement, cycle time, feed quality and control system all influence the final performance of the plant.
For example, in an oxygen PSA system, compressed air is passed through an adsorbent such as a zeolite molecular sieve. Nitrogen is preferentially adsorbed, while oxygen-enriched gas passes through as the product. In a nitrogen PSA system, carbon molecular sieve can be used to preferentially adsorb oxygen and other components, allowing nitrogen-rich gas to be produced.
Therefore, the term PSA plant does not describe only one specific machine. It represents a family of systems designed around the same pressure-swing adsorption principle but configured for different gas-separation requirements.
What Is a PSA Plant?
A PSA plant is an integrated system designed to separate or purify gases using adsorption and pressure changes. The plant normally contains one or more adsorption vessels filled with an appropriate adsorbent material.
The feed gas first goes through a pre-treatment stage. This stage is extremely important because dust, moisture, oil and other contaminants can affect the adsorbent and other internal components. After treatment, the feed gas enters the adsorption vessel under controlled pressure.
Inside the vessel, the adsorbent selectively captures certain components of the feed gas. The desired product gas continues toward the outlet while the unwanted components remain temporarily attached to the adsorbent.
After the adsorption stage reaches its required point, the vessel is depressurized. The reduction in pressure allows the adsorbed components to be released. This process restores the adsorption capacity of the material so that it can be used again.
A typical PSA system therefore operates through repeated cycles of:
- Feed gas preparation
- Pressurization
- Adsorption
- Product gas collection
- Depressurization
- Regeneration
- Re-pressurization
Main Components of a PSA Plant
A PSA plant contains several interconnected components. Each component has an important role in ensuring stable and efficient operation.
Pre-Filter and Feed Gas Treatment System
The pre-filter is generally installed before the adsorption section. In the image, the blue vertical vessel represents the filtration section of the system.
The purpose of the pre-filter is to remove unwanted particles and contaminants from the feed gas before it reaches the adsorption vessel. Depending on the application and feed conditions, additional treatment equipment such as moisture separators, dryers, oil-removal filters and other filtration stages may be required.
Proper feed-gas treatment is particularly important because adsorption materials can be sensitive to contaminants. Excessive moisture or oil contamination can reduce adsorption performance and may shorten the useful life of the adsorbent.
A good filtration system can therefore contribute to:
- Better adsorbent protection
- More stable operation
- Improved product quality
- Reduced contamination
- Longer equipment life
- Lower maintenance requirements
Adsorption Vessel
The large yellow vessel shown in the image represents an adsorption tower or adsorption vessel. This is one of the most important parts of the PSA system.
The vessel contains a bed of specially selected adsorbent material. The adsorbent is selected according to the gas-separation requirement.
During the adsorption phase, the feed gas enters the vessel and passes through the adsorbent bed. Specific gas molecules are preferentially retained by the adsorbent while the desired product gas passes through.
The vessel must be designed to withstand the required operating pressure and provide suitable gas distribution through the adsorbent bed.
Adsorbent Material
The adsorbent is the heart of a PSA system because the separation process depends on its selective adsorption characteristics.
Different applications require different adsorbents. Common examples include molecular sieves, zeolites and carbon molecular sieves.
The selection depends on:
- Type of feed gas
- Desired product gas
- Required purity
- Operating pressure
- Required recovery
- Moisture conditions
- Temperature
- Process configuration
The adsorbent should be properly loaded and protected because channeling, contamination, moisture and mechanical damage can affect its performance.
Automatic Valves
A PSA plant requires accurate switching between different stages of the cycle. Automatic valves are therefore an essential part of the system.
The valves control the direction and timing of gas flow between adsorption vessels, feed lines, product lines and regeneration or exhaust lines.
Because PSA operation involves repeated pressure changes, valve reliability is very important. A valve that does not open or close correctly can disturb the intended cycle and affect product quality and plant performance.
Process Piping
The interconnected piping shown throughout the image provides pathways for gas movement between the different parts of the PSA system.
Piping must be properly designed to handle the operating pressure and gas flow requirements. It should also minimize unnecessary pressure losses and provide appropriate connections for valves, instruments and maintenance.
The pipe layout depends on the number of adsorption vessels and the specific PSA process configuration.
Pressure Gauges
Pressure gauges are used to monitor pressure conditions at various locations in the system.
Pressure monitoring helps operators understand whether the PSA plant is operating within the intended range. Abnormal pressure changes can indicate problems such as valve malfunction, blockage, leakage or incorrect operating conditions.
Additional electronic pressure transmitters can also be connected to the control system for automatic monitoring.
Control Panel
The control panel shown in the image is responsible for managing and monitoring the PSA process.
A modern PSA plant can use PLC-based automation to control valve sequencing and cycle timing. The control system can monitor different operating parameters and generate alarms when abnormal conditions are detected.
A control panel may include:
- PLC control system
- HMI display
- Pressure indicators
- Status lights
- Start/stop controls
- Emergency stop
- Alarm indicators
- Automatic/manual operating modes
Automation helps reduce the need for constant manual intervention and allows the PSA cycle to be repeated consistently.
How Does a PSA Plant Work?
The working principle of a PSA plant is based on selective adsorption and pressure variation. Although the exact cycle differs between applications, the basic process can be understood through several stages.
Feed Gas Entry
The process begins when the feed gas enters the plant. In an air-separation application, atmospheric air is compressed before being introduced into the PSA system.
The compressed feed gas first passes through the required filtration and treatment equipment.
The quality of the incoming gas is important because contaminants can negatively affect the adsorption material and downstream equipment.
Pressurization Stage
After feed preparation, the adsorption vessel is brought to the required pressure.
The pressure level depends on the specific PSA application, adsorbent and process design. Once the vessel reaches the appropriate operating condition, the adsorption stage begins.
Adsorption Stage
During adsorption, the feed gas flows through the adsorbent bed.
The adsorbent selectively captures certain components of the gas mixture. The desired gas passes through the bed and leaves the vessel as product gas.
For example, in an oxygen PSA process, nitrogen is preferentially adsorbed by the zeolite molecular sieve, allowing oxygen-enriched gas to pass through.
In nitrogen PSA, carbon molecular sieve can preferentially adsorb oxygen, allowing nitrogen-rich gas to pass through.
Product Gas Collection
The desired gas leaving the adsorption vessel is collected and directed toward the product-gas line.
Depending on the installation, the product gas may be sent directly to the application point or first collected in a buffer or storage vessel.
A buffer tank can help smooth out the cyclic nature of PSA production and maintain a more stable supply.
Depressurization
After the adsorbent approaches its loading capacity, the vessel is depressurized.
Reducing the pressure decreases the adsorbent's ability to retain the previously captured components. These gases can then be released from the adsorption bed.
Regeneration
The regeneration stage restores the adsorption capacity of the material.
Depending on the PSA design, regeneration may use pressure reduction, purge gas, pressure equalization or a combination of different process steps.
The regeneration stage is essential because the adsorbent must be prepared for the next adsorption cycle.
Re-Pressurization
After regeneration, the vessel is gradually brought back toward the required adsorption pressure.
It is then ready to begin another adsorption cycle.
In a multi-bed PSA plant, different vessels operate at different stages simultaneously. This arrangement allows the overall plant to produce gas continuously even though each individual vessel operates in a cyclic manner.
PSA Plant Process Flow
| Stage | Process | Main Function |
|---|---|---|
| 1 | Feed Gas | Supplies the gas mixture |
| 2 | Filtration | Removes contaminants |
| 3 | Pressurization | Brings vessel to operating pressure |
| 4 | Adsorption | Selectively captures unwanted gases |
| 5 | Product Collection | Collects desired gas |
| 6 | Depressurization | Reduces vessel pressure |
| 7 | Regeneration | Restores adsorbent capacity |
| 8 | Re-Pressurization | Prepares vessel for next cycle |
Types of PSA Plants
PSA technology can be configured for different gas-generation and purification applications. The equipment design changes according to the desired product gas and feed-gas composition.
Oxygen PSA Plant
An oxygen PSA plant produces oxygen-enriched gas from compressed atmospheric air.
Zeolite molecular sieve is commonly used as the adsorbent. During the adsorption phase, nitrogen is preferentially retained while oxygen passes through as the product stream.
Oxygen PSA systems can be used in several industrial and healthcare-related applications, subject to the required specifications and applicable standards.
Nitrogen PSA Plant
A nitrogen PSA plant produces nitrogen-rich gas from compressed air.
Carbon molecular sieve is commonly used in nitrogen-generation PSA systems. The adsorbent preferentially captures oxygen and allows nitrogen to pass through.
Nitrogen is useful in applications where an inert or low-oxygen environment is required.
Hydrogen PSA Plant
PSA technology can also be used for hydrogen purification.
In hydrogen purification systems, the feed gas can contain hydrogen along with other gases. Suitable adsorbents selectively remove impurities while hydrogen passes through as the product gas.
Hydrogen PSA systems are widely associated with industrial hydrogen purification processes.
Biogas Upgrading PSA System
PSA technology can also be used in biogas treatment and upgrading applications.
Biogas contains methane along with carbon dioxide and other components. A properly designed adsorption process can selectively separate certain components to produce a methane-rich gas stream.
The actual process configuration depends on feed composition, required methane recovery, product specifications and selected adsorbent.
Key Advantages of PSA Technology
PSA systems provide several benefits when properly designed for the intended application.
Continuous Gas Availability
Although adsorption is a cyclic process, multiple vessels can be operated in sequence. This arrangement allows the overall system to provide a continuous product stream.
Automatic Operation
Modern PSA plants can be automated using PLC and HMI systems. Automatic valve sequencing reduces manual intervention and allows repeatable operation.
Compact Industrial Design
PSA systems can provide gas separation without requiring cryogenic temperatures. This can make them suitable for applications where on-site gas generation is preferred.
Flexible Capacity
PSA plants can be designed for different gas-flow requirements. The number and size of adsorption vessels can be selected according to the required production capacity.
Reduced Dependence on Cylinder Supply
For suitable applications, on-site PSA gas generation can reduce dependence on externally supplied cylinders or bulk gas deliveries.
Suitable for Multiple Applications
The same basic PSA principle can be adapted for:
- Oxygen generation
- Nitrogen generation
- Hydrogen purification
- Biogas upgrading
- Industrial gas purification
- Specialized gas separation
Factors Affecting PSA Plant Performance
The performance of a PSA plant depends on several process and equipment parameters.
Feed Gas Quality
The quality of feed gas is one of the most important factors. Excessive moisture, oil and particulate contamination can affect adsorbent performance.
Adsorbent Selection
The correct adsorbent must be selected according to the gas-separation requirement. Different adsorbents have different selectivity and adsorption characteristics.
Operating Pressure
Pressure directly influences adsorption behavior. The operating pressure must therefore be carefully selected during system design.
Cycle Time
PSA operation depends on precisely controlled cycle timing. If adsorption or regeneration periods are not properly optimized, separation performance can be affected.
Valve Performance
Automatic valves must operate reliably because the process depends on repeated switching between different flow paths.
Product Purity
Higher product purity requirements may affect recovery, energy consumption and overall process economics. Therefore, the PSA plant should be designed according to the actual product specification rather than using unnecessarily high purity requirements.
PSA Plant Maintenance
Regular maintenance is essential for keeping the PSA system reliable and efficient. Preventive maintenance should be carried out according to the manufacturer's recommendations and applicable safety requirements.
Filters should be inspected regularly and replaced when necessary. Pressure gauges and transmitters should be checked to ensure accurate readings.
Automatic valves should be inspected for leakage, abnormal noise, slow operation or improper switching. Since valves operate repeatedly during PSA cycles, their condition can have a direct effect on plant performance.
The piping system should also be inspected for leakage, corrosion, loose connections and other abnormalities.
Important maintenance activities can include:
- Checking feed filters
- Inspecting valves
- Checking pressure gauges
- Inspecting piping connections
- Checking control-panel indicators
- Verifying PLC operation
- Checking alarms
- Monitoring product-gas quality
- Inspecting pressure vessels
- Following scheduled adsorbent maintenance or replacement requirements
Importance of Proper Filtration in a PSA System
Filtration deserves special attention because the adsorbent is a critical and relatively sensitive component of the PSA process.
If oil or moisture enters the adsorption vessel in excessive quantities, it can affect the adsorbent's surface and adsorption capacity. Particulate contamination can also create pressure-drop problems or affect flow distribution.
For this reason, the feed-treatment section should be designed according to the compressor output and required gas quality.
A complete pre-treatment system may include multiple stages depending on the application.
PSA Plant Safety Considerations
A PSA plant works with pressurized gases and pressure vessels, so safety must always be an important part of system design and operation.
Pressure vessels and process piping should be designed and installed according to applicable regulations, standards and engineering requirements.
Operators should also receive suitable training and follow the manufacturer's operating instructions.
Important safety considerations include:
- Appropriate pressure-relief arrangements
- Proper isolation facilities
- Regular pressure-equipment inspection
- Leak inspection
- Correct valve operation
- Instrument calibration
- Safe gas-venting arrangements
- Emergency shutdown provisions
- Proper operator training
- Preventive maintenance
The exact safety requirements depend on the gas being handled, operating pressure, plant location and applicable local regulations.
Industrial Applications of PSA Technology
PSA technology is used in a wide range of industries because different adsorbents and process configurations can be selected for different gas-separation requirements.
Healthcare Applications
Oxygen PSA technology can be used in oxygen-generation systems where suitable purity, flow and quality requirements are met.
Manufacturing Industries
Nitrogen generation can support manufacturing processes where an inert atmosphere is required.
Chemical Industry
PSA systems can be used for gas purification and recovery in chemical processing operations.
Oil and Gas Industry
PSA technology can be incorporated into gas purification and hydrogen-related processes.
Biogas and Renewable Energy
PSA systems can be used as part of biogas upgrading processes to separate unwanted components from methane-rich gas.
Food and Packaging
Nitrogen generated through PSA technology can be used in applications requiring controlled atmospheres, depending on product and process requirements.
PSA Plant vs Traditional Gas Supply
For some industrial users, on-site PSA generation can provide operational advantages compared with depending entirely on externally delivered gas.
With traditional cylinder-based supply, users may need to manage cylinder storage, transportation, replacement and delivery schedules.
An appropriately sized PSA plant can instead generate the required gas on-site. This can be particularly useful for facilities with continuous gas demand.
However, the best option depends on production capacity, gas purity, operating hours, electricity cost, maintenance requirements and the economics of the specific application.
How to Select the Right PSA Plant
Selecting a PSA plant should begin with a clear understanding of the required process conditions.
The supplier or system designer generally needs information such as:
- Required gas type
- Required gas purity
- Required flow rate
- Feed-gas pressure
- Feed-gas composition
- Operating hours
- Installation location
- Available utilities
- Required outlet pressure
- Product-gas application
- Expected future capacity
Providing accurate process information helps ensure that the PSA system is appropriately sized rather than being unnecessarily oversized or undersized.
Why Automation Is Important in PSA Plants
Automation is one of the most important features of a modern PSA system.
The PSA process requires repeated switching between adsorption and regeneration. Manual operation would be difficult and inconsistent for a continuously operating industrial system.
A PLC can control the sequence automatically while the HMI provides information about plant status and operating conditions.
Automation can help with:
- Valve sequencing
- Cycle timing
- Pressure monitoring
- Alarm generation
- Start/stop control
- Operating-status indication
- Fault detection
- Process monitoring
A properly configured control system can improve consistency and make operation easier for trained personnel.
Frequently Asked Questions About PSA Plants
What is a PSA plant?
A PSA plant is a gas-separation or gas-purification system that uses selective adsorption and pressure changes to separate components from a gas mixture.
What does PSA stand for?
PSA stands for Pressure Swing Adsorption.
What is the main purpose of a PSA system?
The main purpose is to produce or purify a specific gas by selectively adsorbing unwanted components from a gas mixture.
What is inside a PSA adsorption vessel?
An adsorption vessel contains a specially selected adsorbent material. Depending on the application, this may include zeolite molecular sieve, carbon molecular sieve or another suitable adsorbent.
How does an oxygen PSA plant work?
An oxygen PSA plant uses compressed air and a suitable adsorbent, commonly zeolite molecular sieve. Nitrogen is preferentially adsorbed, allowing oxygen-enriched gas to pass through as the product.
How does a nitrogen PSA plant work?
A nitrogen PSA plant generally uses carbon molecular sieve to preferentially adsorb oxygen from compressed air, allowing nitrogen-rich gas to pass through.
Why is a pre-filter required?
A pre-filter helps protect the adsorption material by removing contaminants from the feed gas before it enters the adsorption vessel.
Is PSA an automatic process?
Modern PSA plants can be highly automated using PLC-based control systems and automatic valves.
How many vessels are required in a PSA plant?
The number of vessels depends on the process design, required capacity, cycle configuration and product-gas requirements. Multi-vessel systems allow different adsorption beds to operate at different stages of the cycle.
How often should a PSA plant be maintained?
Maintenance frequency depends on the equipment design, operating hours, feed-gas quality and manufacturer's recommendations. Filters, valves, instruments and other components should be inspected periodically.
Can PSA technology be used for biogas?
Yes. PSA can be used in certain biogas upgrading configurations to separate components such as carbon dioxide from methane-rich gas.
Is PSA technology suitable for industrial applications?
Yes. PSA technology is used across many industries for gas generation, purification and separation, provided the system is properly designed for the specific application.
Conclusion
A PSA Plant is a versatile gas-separation and purification technology that can provide an efficient solution for industries requiring reliable gas production or purification. Its operation is based on the selective adsorption of gas components and controlled pressure changes.
The system shown in the image demonstrates the major equipment associated with an industrial PSA installation, including a pre-filter, adsorption vessel, automatic valves, pressure gauges, control panel and interconnected piping. Each component has a specific function, and the overall performance of the plant depends on how effectively these components work together. https://www.indiamart.com/
The adsorption vessel contains the key adsorbent material, while the pre-filter helps protect the adsorption bed from contaminants. Automatic valves manage the cyclic gas flow, pressure gauges and instruments provide process information, and the control panel coordinates the operating sequence.
PSA technology can be applied to oxygen generation, nitrogen generation, hydrogen purification, biogas upgrading and various industrial gas-treatment requirements. The exact design should always be based on the feed-gas characteristics, required product purity, flow rate, pressure, operating conditions and application requirements.
With suitable engineering, high-quality components, effective filtration, reliable automation and regular maintenance, a PSA system can provide a dependable on-site gas-generation or purification solution for many industrial applications.
Leave A Comment